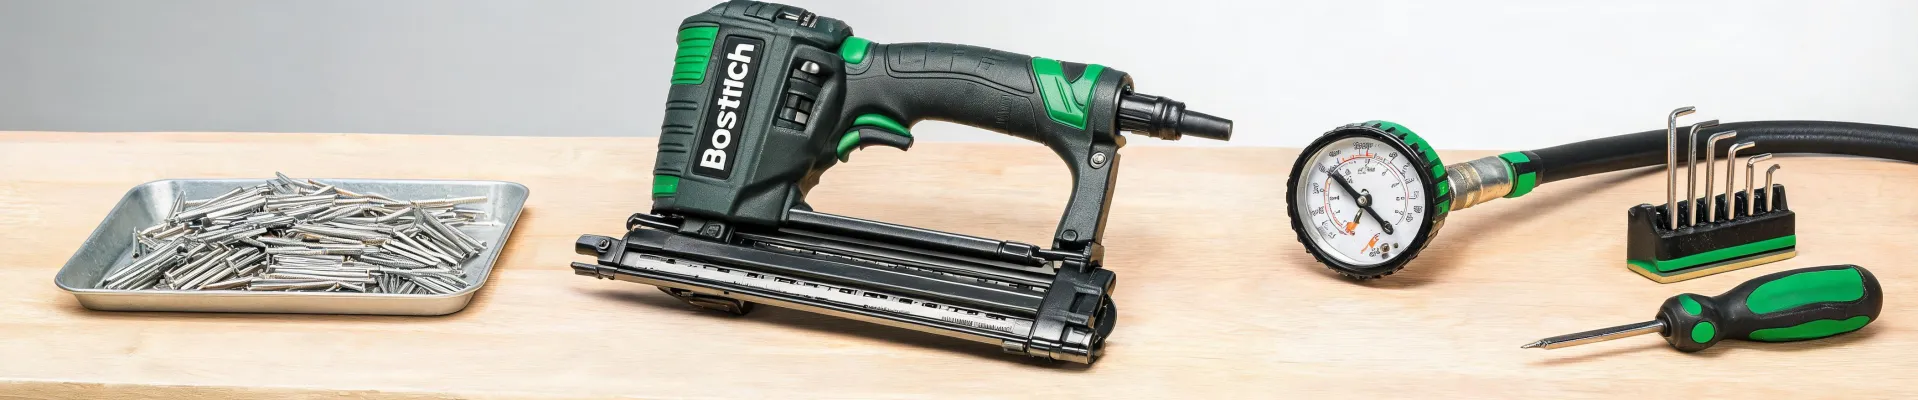
At 6:42 a.m. in March 2024, my phone rang. A finish crew was already on site. They had a Bostitch stapler that would not return after each shot, a trim package due by noon, and a client walking the house at 1 p.m. The problem was not the compressor. It was not the nail gun. It was a return spring that costs less than lunch. The exact part? A Bostitch stapler spring replacement (model-specific, of course). We found one at a supply house 22 miles away. We paid $18 for the spring and $85 for a courier. The crew lost 90 minutes. That one small part put a $12,000 trim job on the edge of a callback.
If you buy tools for a living, you have probably had a version of this. The tool is not the issue. The system around the tool is.
The surface problem: it always looks like a broken tool
When a Bostitch stapler stops returning, the first assumption is usually that the stapler is done. Same with a nail gun that misfires. Same with a chainsaw that will not oil. From the outside, it looks like a machine failure. The reality is that most emergency downtime comes from one small component, one wrong spec, or one missing part in the crib.
I have seen a crew throw away a perfectly good Bostitch stapler because they did not know a Bostitch stapler spring replacement was a 10-minute repair. I have also watched a maintenance tech spend two hours diagnosing a Stanley Bostitch nail gun parts issue when the actual fix was a $4 bumper and an O-ring. The tool was fine. The parts system was not.
The deeper cause: small parts are treated as commodities
Here is the part that most procurement teams miss. Fasteners and repair parts are not commodities. A #8 machine screw is not just a #8 machine screw. A star drive trim-head finish screw is not just a trim screw. A 358 chainsaw parts order is not just a parts order. Each one has a specification stack: diameter, thread pitch, length, head type, drive size, material, coating, and fit class.
Take the question I get at least once a month: what size drill bit for #8 machine screw? The honest answer is: it depends. If you are tapping a #8-32 thread, the common tap drill is a #29 bit. If you need a clearance hole, you might use a #18 or 11/64 inch bit, depending on how tight the fit needs to be. If the screw is #8-40, the answer changes. If you grab the wrong bit, you either strip the threads or drill a hole so loose the joint will not hold. Then the job stops, and someone runs to the truck for a bigger screw that does not match the hardware schedule.
The same problem shows up with star drive trim-head finish screws. People assume all star drives are the same. They are not. A T10, T15, and T20 are different sizes. Use the wrong bit and you cam out the head. Now you are extracting a screw from finished trim, which is a much worse job than driving it in the first place. In my opinion, the label on the screw box is not a suggestion. It is the minimum information you need.
And this is where the value-over-price argument gets real. The lowest unit price on a box of trim screws or a bag of Bostitch parts can be the most expensive decision on the job. I only believed that after ignoring it once. We saved about $60 on a cheaper parts order. The parts looked close enough. Two were not. We lost a half-day, paid $300 in rush shipping to replace them, and ate a $680 labor overrun. That $60 savings turned into a $980 problem. I have not made that mistake since.
The hidden cost: downtime math changes everything
People think rush orders cost more because the parts are rare. Actually, rush orders cost more because they disrupt planned workflows. The part itself is often cheap. The disruption is not.
Run the numbers on a typical trim crew. Four people on site. Loaded labor rate, conservatively, $65 per person per hour. If they stand around for two hours because a Bostitch stapler spring replacement is missing, that is $520 in labor before you add anything else. Add a foreman call, a supply run, and an expedited shipping charge. Add the risk of a missed inspection or a client walk-through. Now the $12 spring is attached to a $1,500 problem.
I have handled 200+ rush parts orders over the last eight years, mostly for commercial finish and remodel crews. The pattern is always the same. The emergency is rarely caused by a catastrophic failure. It is caused by a small, predictable wear item that nobody stocked because it looked too cheap to matter. A Bostitch stapler spring. A Stanley Bostitch nail gun parts kit with the wrong O-ring. A star drive bit that snapped because it was the wrong size. A 358 chainsaw parts order that was placed by model number from memory instead of from the serial plate.
From the outside, a well-run tool crib looks like shelves of small parts. The reality is that it is a risk-management system. The shelves are not inventory. They are insurance.
What actually prevents the emergency
The fix is not complicated, but it does require treating small parts like production equipment.
1. Build a critical spares kit for your most-used tools. For Bostitch staplers and nailers, that means the parts that fail under heat and cycle count: return springs, bumpers, O-rings, trigger valves, driver blades, and magazine springs. If you run Bostitch staplers daily, keep a Bostitch stapler spring replacement for each model you own. For Stanley Bostitch nail gun parts, order by model and serial number from the parts diagram. Do not trust a photo. Do not trust a lookalike.
2. Stock the fasteners and bits you actually use. If your trim package calls for star drive trim-head finish screws, keep the right T10, T15, or T20 bits in every install bag. Then keep a backup box of the exact screws. A mismatched screw is not a shortcut. It is a callback waiting to happen.
3. Treat 358 chainsaw parts like any other production-critical part. Log the exact model and serial. Keep the common wear items: air filter, fuel filter, spark plug, sprocket, bar nuts, and oil lines. If a saw goes down during a clearing or demo job, the difference between a 20-minute fix and a two-day parts order is usually a $15 filter and a $30 sprocket.
4. Answer the drill bit question before the drill comes out. For a #8-32 machine screw, a #29 tap drill is the standard starting point. For clearance, check the fit class and use a #18 or 11/64 inch bit as a common starting point. ASME B1.1 defines the unified inch screw thread system, so if the thread callout is #8-32, it is not the same as #8-40. When in doubt, test on scrap. That is cheaper than fixing a stripped hole in finished work.
5. Compare total cost, not unit price. I get why people go with the cheapest option. Budgets are real. But the lowest quote often hides the cost of wrong parts, delayed deliveries, and rework. A parts supplier that costs 10% more but ships the right part today is usually cheaper than the one that saves you $12 and costs you a day.
The point
The job does not fail because the nail gun is bad. It fails because the system around the nail gun treats a $12 spring, a $6 drill bit, and a box of trim screws as afterthoughts. If you run crews, fix the system. Stock the wear parts. Verify the spec. Check the model number. Answer the drill bit question before you drill. Then the tool can do what it was bought to do, and you can stop paying emergency prices for ordinary parts.
Leave a Reply